

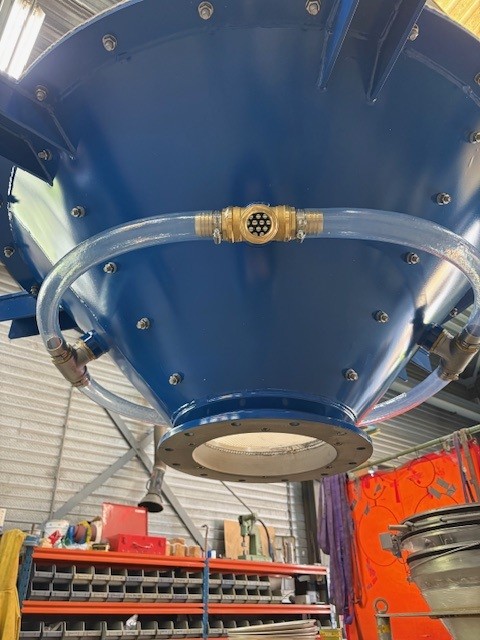
Fluidised sub-cone for optimum production flow
Veenstra has supplied a bespoke silo conversion for an existing production site in the plastics/polymers industry, in which the old vibrating floor has been replaced by a fluidised bottom cone. This upgrade has resulted in a significantly improved product outflow and prevents blockages that occurred regularly in the previous setup.
Read more
Project scope: fluidisation and silo optimisation
Veenstra carried out the entire process, from design and production through to delivery and commissioning of the new sub-cone. The customer modified the existing silo outlet in accordance with our technical specifications, after which our team tested the system and brought it into operation. The new system consists of the following main components:
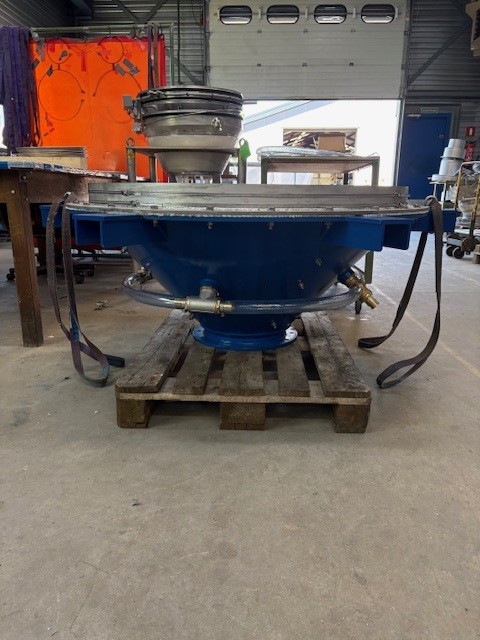
- Fluidised sub-cone, Ø1200mm top connection – Ø300mm bottom connection, H=600mm*
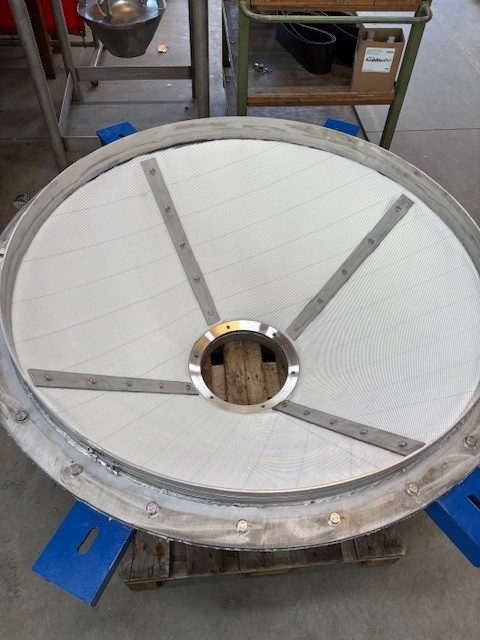
- Outer cone with 3/4 internal sections fitted with breathable fabric
- Air distributor and pressure regulator
- Air hoses and all necessary fittings
- Counter-flange with rubber sleeve for connection to the existing silo
- New manual valve for maintenance, fitted between the lower cone and the screw conveyor
Challenges in the existing silo outflow
In the original set-up, the vibrating floor beneath the silo regularly caused blockages and downtime. The existing pads provided only limited support, as virtually no effective fluidisation took place in the vibrating floor. Due to the relatively flat cone angle, materials tended to get stuck, making the outflow unpredictable and resulting in more frequent maintenance. This led to inefficient material throughput and, ultimately, low operational reliability.
Solution with a fluidised lower cone
Veenstra has replaced the entire vibrating floor with a fluidised lower cone with a steeper angle of repose, ensuring that the product is loosened evenly and flows continuously towards the screw conveyor. By also upgrading the feed chute above the conveyor, additional height could be utilised to ensure an optimal product flow. This bespoke solution ensures a stable, trouble-free outflow, reduced maintenance, lower downtime costs and significantly greater operational reliability.